
Why Do Your Tension Polyurethane Screen Panels Keep Failing?
Your screening operation is running slow, and unexpected downtime is killing your profits. Understanding why your <a href="/tag/tension-screen" target="_blank"><strong>tension <a href="/tag/screen" target="_blank"><strong>screen</strong></a></strong></a>…
Your screening operation is running slow, and unexpected downtime is killing your profits. Understanding why your <a href="/tag/tension-screen" target="_blank"><strong>tension <a href="/tag/screen" target="_blank"><strong>screen</strong></a></strong></a> panels fail is the first step to choosing a better, more reliable product.
The most common failures in tension <a href="/tag/polyurethane-screen-panels" target="_blank"><strong><a href="/tag/polyurethane-screen" target="_blank"><strong><a href="/tag/polyurethane" target="_blank"><strong>polyurethane</strong></a> screen</strong></a> panels</strong></a> include aperture deformation, hook breakage, surface tearing, and blinding or pegging. These issues are caused by a combination of material wear, high impact, improper installation, and environmental factors like moisture, ultimately reducing screening efficiency and panel lifespan.
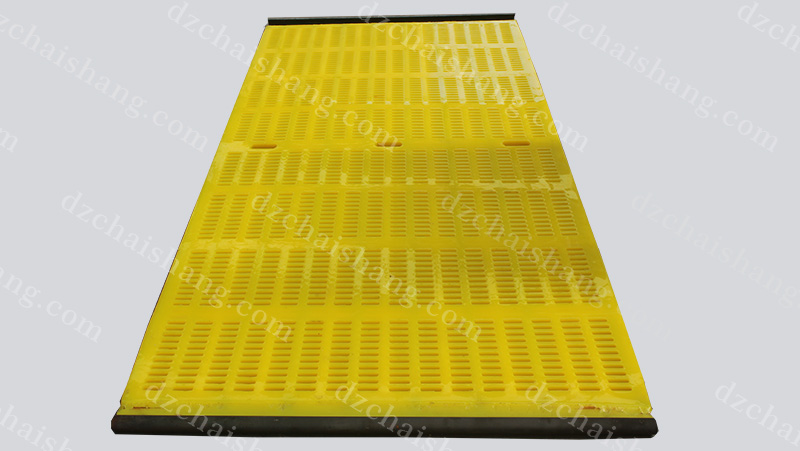
I've been in this business for a long time, and I've seen just about every way a screen panel can fail. It's frustrating for operators because a failed panel means a complete halt to production. But these failures aren't random. They are predictable, and more importantly, they are often preventable if you know what to look for. By understanding the root cause of each failure mode, you can work with your supplier to specify a panel that is truly built for your specific application. Let's break down the most common problems I see in the field.
Why Do Screen Panel Apertures Deform Over Time?
Your final product suddenly isn't meeting size specifications, leading to rejected batches. The cause is often gradual aperture deformation, a sneaky problem that compromises your quality without a catastrophic failure.
Apertures deform due to the constant impact and abrasion from processed materials. This continuous stress, combined with the polyurethane's natural elasticity, can cause the holes to stretch or change shape permanently over time, especially if the polymer quality is low or the panel is poorly designed.

When I visit a site and see out-of-spec material, the first thing I check is the screen apertures. A brand-new panel has perfectly shaped holes. But after weeks of being pounded by rock and ore, things start to change. The <a href="/tag/polyurethane-material" target="_blank"><strong>polyurethane material</strong></a> has a "memory," meaning it's supposed to flex and return to its original shape. However, under relentless attack, this memory can fade. The holes start to stretch, especially at the feed end of the screen deck where the impact is greatest. This isn't just about wear; it's about the polymer itself losing its structural integrity. A low-quality polyurethane will deform much faster than a premium, high-resilience formula. It's a critical detail that separates a panel that lasts three months from one that lasts a year.
Key Factors Causing Aperture Distortion
Several factors work together to warp the apertures. Understanding them helps in specifying the right panel.
| Factor | Impact on Aperture | How to Prevent It |
|---|---|---|
| High Abrasion Material | Sharp or hard particles slowly wear down the edges of the holes, effectively making them larger. | Specify a polyurethane formula with a high abrasion-resistance rating for your specific material. |
| Heavy Impact Load | Large, heavy material falling from a height can stretch the polyurethane beyond its elastic limit. | Ensure the panel thickness and durometer (hardness) are matched to your top-size material and drop height. |
| Poor PU Quality | A low-grade polymer has poor elastic memory and will take on a permanent stretch much sooner. | Always source from a reputable manufacturer who can provide data on their polymer's physical properties. |
| Incorrect Tensioning | If the panel is tensioned unevenly, it creates constant stress points that pull certain apertures out of shape. | Train your maintenance team on proper, even tensioning procedures for your specific screen box. |
What Causes the Hooks on Tension <a href="/tag/screens" target="_blank"><strong>screens</strong></a> to Break?
Your screen deck suddenly starts making a terrible noise, and you find a panel has come loose. This immediate shutdown is a huge headache, and the culprit is often a broken hook.
Hooks on tension screens typically break for two reasons: poor bonding between the polyurethane and the internal steel reinforcement, or metal fatigue from the machine's constant vibration. Low-quality steel or improper manufacturing processes significantly accelerate this type of failure, causing premature breakdowns.

A tension screen panel is only as strong as its hooks. I've seen perfectly good screen surfaces rendered useless because a hook snapped off. This is almost always a manufacturing issue. During production, the steel hook needs to be perfectly prepared and chemically bonded to the liquid polyurethane as it's being molded. If this bond is weak, vibration will cause the polyurethane to delaminate from the steel. Once that separation starts, the hook flexes independently and eventually fatigues and breaks. The other cause is simply using cheap steel. A hook has to endure millions of vibration cycles under tension. Using a lower-grade steel that isn't designed for this kind of dynamic load is a guaranteed way to ensure it will fail early. This is one area where you absolutely cannot cut corners.
Analyzing Hook Failure: Bonding vs. Material Fatigue
When a hook fails, it’s crucial to know why. It tells you a lot about the manufacturer's quality control.
| Failure Point | Root Cause | Manufacturer's Responsibility | Operator's Role |
|---|---|---|---|
| Delamination | The polyurethane pulls away from the steel hook. This points to a weak chemical bond from the factory. | Use proper surface preparation and chemical primers on the steel before molding. | This is a manufacturing defect; the operator can't prevent it. |
| Metal Fatigue | The steel hook itself snaps, usually at a bend or stress point. This is caused by repeated flexing. | Select high-endurance, fatigue-resistant steel for the hook reinforcement. | Ensure correct tensioning. Overtightening the panel dramatically increases stress and accelerates fatigue. |
| Corrosion | In wet screening applications, rust can form on the steel, weakening it until it breaks. | Use stainless steel or apply corrosion-resistant coatings to the hooks. | Perform regular inspections for signs of rust, especially in humid or wet environments. |
How Can You Prevent Surface Tearing on Large Aperture Screens?
You're processing heavy, large-sized ore, and a routine inspection reveals a huge gash in your screen panel. This tear allows oversized material to contaminate your product, forcing a costly shutdown.
Surface tearing, especially on panels with large apertures, is caused by the high-impact energy of large, sharp material. This impact concentrates stress on the thin polyurethane webs between the holes, causing them to rip. Using a panel that is too thin or lacks sufficient tear strength is a primary cause.

I see this problem most often in primary screening applications. When you have large, heavy rocks falling onto a screen, the force is immense. If the screen has large openings, there's very little material—the "webs" between the holes—to absorb that impact. Think of it like a net. A net with small holes is much stronger than a net with huge holes made from the same thickness of rope. It's the same principle here. A sharp-edged rock hitting one of those thin webs can initiate a small cut. With the constant vibration and tension of the screen, that small cut quickly propagates into a massive tear. The solution isn't just to use a thicker panel, though that helps. It's also about the specific polyurethane formula. Some formulas are designed for abrasion resistance, while others are designed for high tear strength. For these applications, you need the latter.
Mitigating Tear Risk in High-Impact Screening
Preventing tears requires matching the panel's design to the harsh reality of the material being processed.
| Contributing Factor | Description | Solution |
|---|---|---|
| Large Particle Size | A heavy rock carries significant kinetic energy, which is transferred to the panel upon impact. | Use a thicker panel to help distribute the load. Also, consider using an impact-absorbing feed plate at the start of the deck. |
| Sharp-Edged Material | Sharp points on rocks and ore act like a knife, concentrating all the impact force on a tiny area. | Specify a polyurethane formula with a high "tear propagation resistance." This means even if a cut starts, it won't easily spread. |
| Large Apertures | The webs between large holes are thinner and weaker, making them the most likely failure point. | Discuss reinforced web designs with your manufacturer. Some panels can be made with thicker webs or internal reinforcement. |
| Low Temperature | In cold climates, polyurethane can become more brittle and less able to absorb impact, making it more prone to tearing. | Ensure your supplier provides a polyurethane grade that is rated for your specific operating temperature range. |
Why Do Your <a href="/tag/screen-panels" target="_blank"><strong>screen panels</strong></a> Suffer From Blinding and Pegging?
Your screening throughput has dropped dramatically, and your team is spending more time cleaning screens than producing. The screen surface is clogged with material, a classic case of blinding and pegging.
Blinding and pegging happen when near-size particles get stuck in the apertures (pegging) or when fine, moist material sticks to the screen surface and blocks the holes (blinding). High moisture content, sticky clay-like materials, and static electricity are the main causes of this efficiency-killing problem.
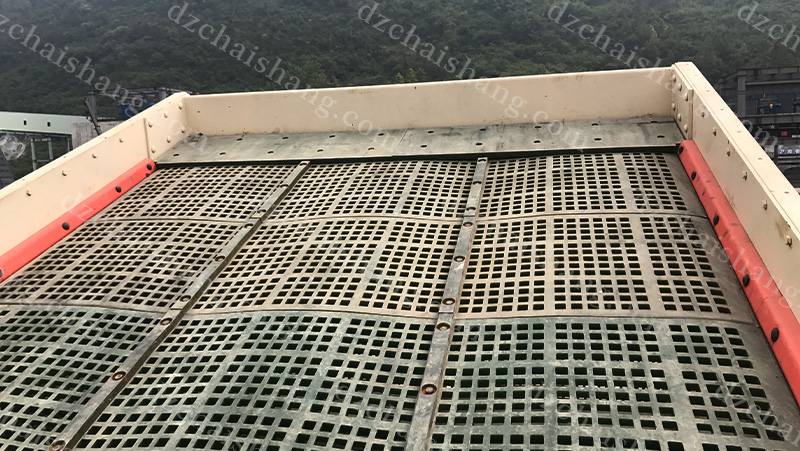
This is one of the most frustrating problems in screening. I've seen operations where efficiency drops by 50% or more because the screen is no longer open. Pegging happens when a rock is just the right size and shape to get wedged tightly in an aperture. Blinding is worse; it's when a whole layer of fine, damp material cakes onto the screen surface like mud. This is very common in rainy weather or when processing materials with high moisture or clay content. The flexibility of polyurethane is supposed to help with this. As the panel vibrates, it creates a "trampoline effect" that actively throws the material up and dislodges stuck particles. However, if the material is too sticky or the panel isn't tensioned correctly, this self-cleaning action fails. A well-designed panel with tapered apertures can make a huge difference here.
Strategies to Combat Blinding and Pegging
An effective screening operation depends on open apertures. Here is how to keep them clear.
| Problem | Key Cause | Solution |
|---|---|---|
| Pegging | Near-size particles (pieces that are very close to the aperture size) become mechanically wedged in the openings. | Use panels with tapered or conical apertures, which are wider at the bottom. Ensure the panel is properly tensioned to maximize the self-cleaning flex. |
| Blinding | Fine, wet, or sticky material adheres to the screen surface, covering the openings. Often caused by moisture or static. | Improve upstream dewatering if possible. A highly flexible panel with a strong vibrating action is essential. Ask about special anti-static PU formulas. |
| High Ambient Humidity | Moisture in the air makes fine dust particles clump together and stick to surfaces. | Maximize the "trampoline effect." The active, trampoline-like motion of a properly tensioned polyurethane screen is your best defense against material buildup. |
Conclusion
Understanding these failures—aperture deformation, hook breakage, tearing, and blinding—is crucial. Choosing a quality manufacturer who designs to prevent them ensures a longer panel life and much better plant efficiency.